








In this article
- What is XYZ analysis in inventory management?
- How to calculate XYZ inventory classes
- 1. Choose the items, history and time periods
- 2. Check what the quantities actually represent
- 3. Calculate the average and coefficient of variation
- 4. Set boundaries and inspect the result
- Worked example: the same average, a different stock decision
- Turn X, Y and Z into different controls
- Combine ABC and XYZ without confusing value with urgency
- Connect replenishment decisions to production with SkyPlanner
- What a shared schedule changed at Mamec
- Start with one material group and two contrasting parts
Home » Resources » XYZ Analysis: Match Stock Control to Demand Patterns
Estimated reading time: 11 minutes
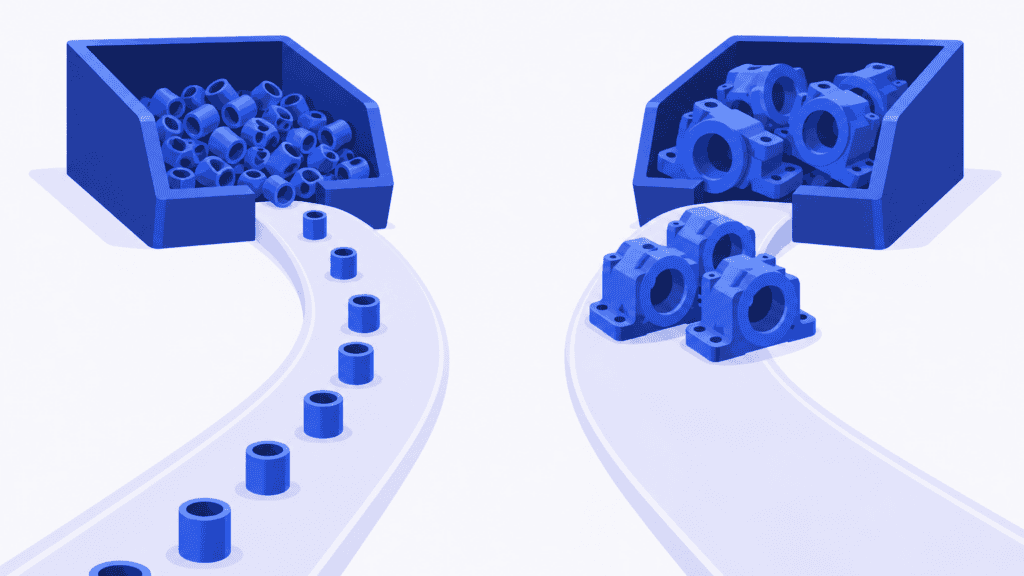
Two components can have the same average usage and need completely different replenishment routines. One leaves stores steadily every week. The other sits untouched until a large customer order consumes several months’ worth at once. Ordering both from the same average invites excess stock on one side and shortages on the other.
XYZ analysis helps you recognise that difference. It groups items by their consumption patterns, so you can separate routine replenishment from the parts that need closer demand review. Combined with ABC analysis, it shows both where the money goes and how reliably usage can be anticipated.
The next step is making the resulting supply decisions work in production. SkyPlanner APS connects material availability with the approved orders and resources that need it, reducing the time you spend reconciling stock information with separate machine queues.
What is XYZ analysis in inventory management?
XYZ analysis classifies inventory items by the variability and regularity of their demand or consumption over time. It helps you choose how to monitor an item and plan its replenishment, rather than applying one control routine to every part.
| Class | Typical consumption pattern | What the planner needs to understand |
|---|---|---|
| X | Relatively steady, with limited variation between periods | Whether routine replenishment remains appropriate as usage and supply change |
| Y | More variable, often with a trend or seasonal pattern | What explains the changes and whether that pattern can be anticipated |
| Z | Irregular or sporadic, sometimes with long gaps between withdrawals | What triggers the next requirement and what a shortage would interrupt |
These classes describe a pattern, not a guaranteed forecast accuracy. A seasonal item may vary strongly across the year yet be quite predictable with a suitable seasonal forecast. A usually steady item can still surprise you when a major customer changes its order.
XYZ also answers a different question from ABC. For manufacturing materials, ABC commonly ranks annual consumption value: quantity used multiplied by unit cost. XYZ examines how that usage is distributed over time. An expensive item is not necessarily unpredictable, and a cheap item is not necessarily steady.
Neither label tells you how critical a missing component is to production. Keep that consequence visible separately.
How to calculate XYZ inventory classes
A common numerical starting point is the coefficient of variation, or CV. It compares the spread of period-by-period consumption with the average consumption. Use it alongside the actual demand pattern, not instead of looking at it.
1. Choose the items, history and time periods
Start with a clearly defined material group, such as purchased components used at one plant. Collect quantities by item and equal-length planning periods, using consistent units. Do not mix pieces, boxes and kilograms within one item’s history.
Choose a period length that helps the decision you are making. Monthly totals may suit a purchasing review, but they can hide weekly peaks that matter for a short replenishment cycle. Daily data may look intermittent simply because production withdraws a week’s requirement in one batch.
Use enough history to see the relevant operating cycle. If seasonality matters, a short run of recent weeks cannot establish the full pattern. Keep the history window and period length consistent when comparing items, and record both so the classification can be reproduced.
2. Check what the quantities actually represent
Purchases arriving in large deliveries are not the same as production consuming material. Use consumption or demand data appropriate to the question, rather than accidentally classifying the supplier’s delivery pattern.
Retain genuine zero-consumption periods. Removing them makes a sporadic item look steadier than it is. Missing records are different: investigate them rather than replacing them with zeroes.
Also check whether shortages suppressed consumption. A week with no issues because the part was unavailable is not evidence that production needed none. New products, discontinued items, stock corrections and unusual one-off projects need explicit review before their history becomes a replenishment rule.
3. Calculate the average and coefficient of variation
For each item, calculate:
Average consumption = total consumption ÷ number of periods
Coefficient of variation = standard deviation of period consumption ÷ average consumption
Standard deviation measures how widely the period quantities vary around their average. Dividing by the average expresses that spread relative to the item’s normal usage, allowing a more useful comparison between items with different consumption volumes.
Keep the standard-deviation convention consistent. The worked example below uses sample standard deviation, calculated with one less than the number of observations in the denominator. Do not switch between sample and population calculations without recording the change.
You can express CV as a ratio or a percentage. A ratio of 0.50 is 50%; it does not mean a 50% chance of a shortage. If average consumption is zero, the division is undefined. If the average is very small, the result can change sharply with a small quantity change. Flag those items for review rather than forcing a precise-looking classification.
4. Set boundaries and inspect the result
There is no universal pair of CV boundaries that guarantees the right inventory policy. State your chosen boundaries, including where an exact boundary value belongs, and test whether the groups distinguish materially different planning needs.
For the illustration below only, use X for CV at or below 0.50, Y for CV above 0.50 and at or below 1.00, and Z for CV above 1.00. These are demonstration rules, not recommended default settings for your factory.
Before adopting the classes, inspect the consumption history. A high CV caused by a repeatable seasonal peak calls for a different response from a high CV caused by isolated, uncertain orders.
Worked example: the same average, a different stock decision
Imagine two components with the following eight weeks of consumption. The short history illustrates the calculation; it is not enough by itself to validate a long-term stocking policy.
| Component | Weekly consumption, weeks 1–8 | Total | Weekly average | Sample standard deviation | CV | Illustrative class |
|---|---|---|---|---|---|---|
| Standard sleeve | 90, 110, 90, 110, 90, 110, 90, 110 | 800 | 100 | 10.69 | 0.11 | X |
| Project housing | 0, 0, 0, 400, 0, 0, 0, 400 | 800 | 100 | 185.16 | 1.85 | Z |
For the sleeve, CV is approximately 10.69 ÷ 100 = 0.11. For the housing, it is approximately 185.16 ÷ 100 = 1.85. Both averages are 100 units per week, but only the sleeve has anything resembling a weekly requirement of that size.
Routine replenishment may work well for the sleeve once lead time and supply reliability are considered. Buying 100 housings every week, however, can build stock during quiet weeks without securing enough for the next project. If a confirmed order requires 400, that order-specific requirement matters more than the average.
The housing history also contains six zero-consumption weeks. For intermittent demand, look at both the size of withdrawals and the gaps between them. CV alone does not tell you when the next withdrawal will occur. In make-to-order work, a confirmed customer order and its material requirements may provide a much stronger planning signal than a statistical average.
Turn X, Y and Z into different controls
The classification is useful when it changes a decision. Give the item group a replenishment approach, an owner and a reason to review exceptions.
For X items, simplify predictable routine work. A reorder-point routine, scheduled call-offs or another standard replenishment arrangement can reduce repeated purchasing decisions. Check that the routine reflects replenishment time and actual usage. X is not permission to eliminate a buffer or assume the supplier will always deliver on time.
For Y items, identify the driver before increasing stock. If usage rises before a recurring production season, plan supply around that pattern rather than buying from the annual average. If the change comes from a new contract or product ramp-up, review the forward requirements with the people responsible for them. A changing pattern needs an explanation, not just a different letter.
For Z items, make the stockholding decision deliberately. Order-specific purchasing can avoid building inventory for uncertain future work when the customer lead time allows it. A critical spare or a long-lead component may still need stock because waiting for replacement would be unacceptable. Z does not mean obsolete, unimportant or safe to leave unavailable.
Across all three groups, consider replenishment lead time, supplier reliability, minimum order quantities, shelf life, substitutes and the consequence of a shortage. The class does not calculate the safety stock or service level you need. Its job is to direct attention toward the right control question.
Combine ABC and XYZ without confusing value with urgency
ABC–XYZ analysis attaches both labels to an item, producing combinations such as AX, AY and AZ through to CX, CY and CZ. The first letter describes its value class; the second describes its consumption pattern.
That distinction helps allocate management effort. An AX item combines significant annual consumption value with relatively steady usage: close financial control can coexist with a routine replenishment process. An AZ item combines significant value with irregular use: purchasing commitments and the next firm requirement deserve closer attention before more cash is tied up in stock.
A CX item can be a good candidate for simple replenishment that reduces administrative work. A CZ item needs a deliberate judgement about whether to stock it at all, but low annual spend does not cancel the risk of a production stoppage.
You do not need nine entirely different procedures just because the matrix has nine cells. Use the combinations to identify meaningful differences, then document the few control policies your team can actually maintain.
Most importantly, do not turn the matrix directly into machine-queue priority. A job using an AX material is not automatically more urgent than a job using a CZ material. Due dates, customer commitments, available materials and competing capacity still determine what production can sensibly do next.
Connect replenishment decisions to production with SkyPlanner
Return to the two components in the example. You have agreed routine replenishment for the sleeve and an order-specific purchase for the housing. Approved production orders using both components now compete for the same machining centre.
The purchasing policies are different, but the production plan must be shared. Knowing when the housing is expected is only half the decision. You also need to know where its operations fit, what work can run beforehand and whether the resulting completion supports the customer commitment.
SkyPlanner APS brings those constraints together. With material-aware scheduling enabled, its scheduling AI, Arcturus, uses material availability alongside workstation capacity, shifts, operation dependencies and the rules you set. The Gantt schedule shows how the work is placed across resources, so you can assess the combined plan rather than manually reconcile each material list with each machine queue.
When expected supply or a priority changes, update the planning information and recalculate. You can then see the effect on the affected order and the other work sharing its resources. This saves queue-rebuilding effort and makes the delivery consequences of a material decision clearer.
You remain in charge of priorities. Arcturus calculates the schedule within your instructions; an XYZ label does not make the commercial decision for you. Demand forecasting and the decision to replenish remain separate from scheduling the work you have approved. SkyPlanner is the choice for connecting that work to material availability and finite production capacity.
SkyPlanner integrates with any ERP or MES through its open REST API. Material balances can be maintained through the integration or in SkyPlanner’s Warehouse module. That lets you connect existing purchasing and item data to production scheduling without starting with an ERP replacement.
What a shared schedule changed at Mamec
Mamec, a manufacturer of industrial mixing equipment and high-tech contract products, faced thousands of interdependent work orders. Supervisors prioritised paper orders from delivery dates, while the ERP’s planning functions did not provide the overall picture they needed.
With SkyPlanner integrated with Oscar ERP, Mamec moved to AI-powered finite scheduling and work queues locked a week at a time. Its customer account reports a clearly lighter planning workload, reduced workstation downtime and better visibility of production load.
That is the practical benefit beyond an item classification: the relationships between jobs become manageable in one plan. For your team, the opportunity is less time rebuilding queues and more time deciding how to protect the commitments that matter.
Start with one material group and two contrasting parts
Choose a manageable group, check the history and agree reproducible classification rules. Review a steady-use part and a sporadic-use part with purchasing and production. Decide what should change in their controls, who owns the decision and when to reassess it.
Track the outcome in terms that matter: shortage interruptions, excess stock and the effort spent chasing exceptions. Revisit the classes when contracts, product mix or consumption patterns change, rather than waiting for an annual exercise to reveal an outdated policy.
Use XYZ analysis to choose the right replenishment attention. Use SkyPlanner to connect the resulting material availability with a production plan the shop can follow.
Book a SkyPlanner demo with two contrasting components and the approved orders that consume them. Bring the current balances, expected supply dates and production routes, and see how they fit alongside the rest of your work. If you prefer to explore first, try SkyPlanner with demo data.
Jussi Mäntylä
Production Planning Specialist, SkyPlanner


