








In this article
- What is FSN analysis?
- How to conduct FSN analysis with manufacturing data
- 1. Choose the period and define what counts as movement
- 2. Check the history before trusting a zero
- 3. Calculate rate, frequency and recency
- 4. Apply explicit local class rules
- FSN analysis example: four parts, four different decisions
- Turn each class into an owned inventory action
- FSN versus ABC, XYZ and inventory aging
- Connect material decisions to a workable SkyPlanner schedule
Home » Resources » FSN Analysis in Manufacturing: Turn Classes Into Action
Estimated reading time: 10 minutes
A component can sit untouched for months and still be the part your next delivery depends on. Another can leave the warehouse every week while excess stock keeps arriving. Movement matters, but it does not tell you everything about what to buy, keep or use next.
FSN analysis separates inventory into fast-moving, slow-moving and non-moving items. Used well, it directs attention toward replenishment, excess-stock review and the exceptions that deserve a closer look. Used as a disposal list, it can remove the very material production needs.
For a manufacturer, the useful outcome is an agreed material decision connected to the production plan. SkyPlanner APS helps with that next step: fitting the approved work around material availability and shared capacity, instead of making you reconcile a stock list with every machine queue by hand.
What is FSN analysis?
FSN analysis classifies inventory by its consumption or movement over a defined period: fast-moving (F), slow-moving (S) and non-moving (N). In manufacturing, the relevant activity is often material issued to or consumed by production, rather than sales of the finished product.
- Fast-moving items are consumed frequently or at a high rate under your chosen classification rule. Their supply needs regular attention.
- Slow-moving items are used less frequently or at a lower rate. Review whether replenishment still matches their actual requirement.
- Non-moving items have no qualifying consumption during the chosen observation window. Investigate why before changing their supply policy.
The class describes observed activity, not business importance. A cheap fastener can be essential to every assembly. A rarely used replacement component can be essential to one valuable order. Neither its price nor its FSN letter tells you when that order should run.
FSN is therefore one input to inventory management, not a substitute for demand, lead-time and criticality decisions.
How to conduct FSN analysis with manufacturing data
Start with a group of parts for which the comparison makes sense. Regular production components, project-specific materials and emergency spares may need different review rules. Mixing them under one cutoff can make normal behavior look like a problem.
1. Choose the period and define what counts as movement
Select a period long enough to capture the normal production cycle. For a seasonal product, include the relevant season. For project materials, look at the project cycle as well as recent months. A short window can flag a change quickly, but it can also miss legitimate intermittent use.
Write down the rule before assigning letters. For example: “Completed material issues to production, by item, over the last six complete months.” Keep planned requirements separate from completed consumption so future jobs do not make an unused item look historically active.
Define how returns from production are treated. Track genuine issues and returns separately so repeated issuing and returning does not inflate usage. Exclude internal bin transfers and inventory-count corrections from the consumption measure: moving a part to another shelf does not mean production used it.
Use the confirmed business event date for the analysis. The date a record was created or imported may not be the date the material was actually issued.
2. Check the history before trusting a zero
Gather the item code, unit of measure, qualifying consumption quantities and dates, current stock and last qualifying issue date. Add notes for stockouts, new introductions, substitutions and changes to the products that use the part.
A recorded zero needs particular attention. If a part was unavailable, production could not consume it even when demand existed. A newly introduced item has little history. A seasonal component may simply be waiting for its next production run.
Keep those exceptions visible. You can report zero observed consumption while flagging the item for review; you should not silently turn that zero into “no future need.”
3. Calculate rate, frequency and recency
These measures answer different questions:
- Consumption rate: qualifying quantity consumed divided by the observation period, expressed in a consistent unit such as pieces per month.
- Consumption frequency: how often qualifying use occurred. Months with consumption can be more useful than raw transaction counts when one system posts a daily total and another posts each withdrawal.
- Recency: the time since the last qualifying consumption event, measured at the review date.
Use rate to understand replenishment volume, frequency to understand regularity, and recency to spot a possible change. Do not rank kilograms, liters and pieces as though they were interchangeable quantities. Even two components measured in pieces can have very different usage per finished product.
A large one-off issue and small weekly issues can produce the same average rate. Looking at frequency and recency alongside it prevents that average from hiding the pattern.
4. Apply explicit local class rules
Choose thresholds that support the decision you need to make. You might classify a comparable component family by the number of months with consumption, then use quantity and recency to decide what needs attention within each class. Another family may be better served by documented issue-frequency or consumption-rate bands.
There is no universal FSN day limit or percentage split that fits every factory. Avoid forcing the bottom share of a ranking into N when those items actually moved. For this analysis, N means no qualifying consumption in the stated window.
Record the period, rule, review date and exceptions with the result. A letter without its measurement basis is difficult to compare at the next review.
FSN analysis example: four parts, four different decisions
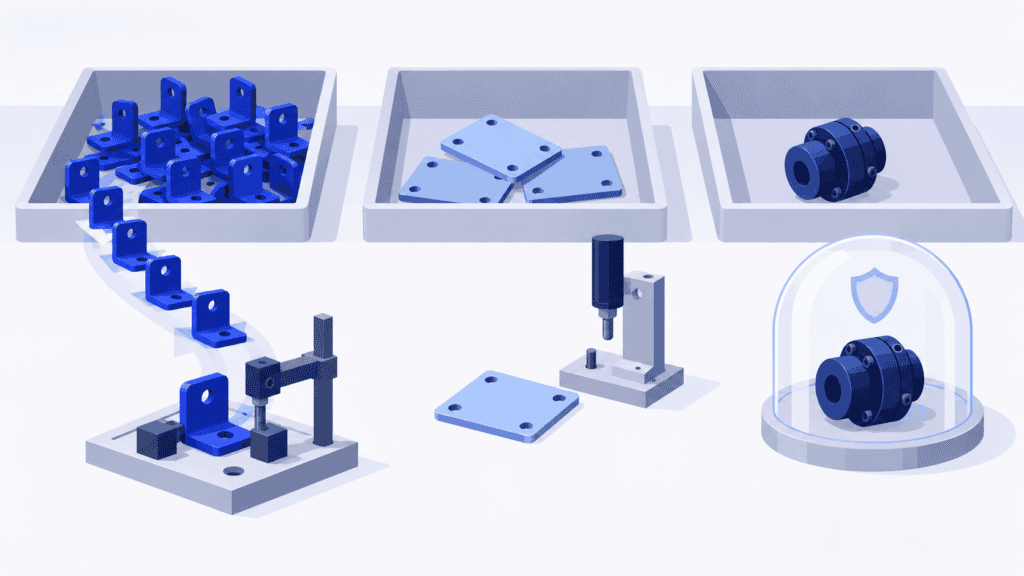
Imagine a manufacturer reviewing one family of assembly components over six complete months. For this example only, it defines F as consumption in four to six months, S as consumption in one to three months, and N as no consumption in the period.
The quantities below are completed production consumption, not planned withdrawals or warehouse transfers.
| Component | Quantity consumed | Months with consumption | Average per month | Observed class | What the team should check |
|---|---|---|---|---|---|
| Standard mounting bracket | 600 pieces | 6 | 100 pieces | F | Does replenishment cover upcoming assembly work and supplier lead time? |
| Special mounting plate | 120 pieces | 2 | 20 pieces | S | Is another approved project due, or are old purchasing quantities creating excess? |
| Critical replacement coupling | 0 pieces | 0 | 0 pieces | N | Is availability still needed for a supported product with a long replacement lead time? |
| Alternate connector | 0 pieces | 0 | 0 pieces | N, review required | Was demand suppressed because the connector was out of stock? |
The mounting plate’s average of 20 pieces a month does not mean it is used every month. Its two active months suggest a different replenishment pattern from the bracket’s regular consumption.
The coupling is non-moving under this local rule, but that is not a reason to discard it. If the business still needs it and cannot replace it in time, retaining an agreed quantity may be the right decision.
The connector needs a data-and-demand review before any reduction. The same recorded zero can mean no demand, unavailable supply or a gap between projects. FSN makes those cases visible; investigation tells you which action is appropriate.
Turn each class into an owned inventory action
For fast-moving items, review replenishment frequency, supplier reliability and the quantities required by upcoming work. Frequent movement can justify accessible storage and closer monitoring. It does not justify unlimited stock: an item can move every week and still be overstocked.
For slow-moving items, compare open purchase orders and purchasing lot sizes with future requirements. A smaller lot, a later delivery or using approved existing stock may be more useful than simply asking production to consume more. Check whether the part is shared across products or tied to one intermittent project.
For non-moving items, establish whether the requirement has ended. Confirm that the item is usable, check remaining product or service commitments, and review replacement lead time and the consequence of a shortage. Possible actions include retaining critical cover, stopping further purchases, using an approved alternative application, returning stock or arranging authorized disposal. The letter alone does not choose among them.
Give the decision an owner and a review date. Purchasing may own the supplier or order change, engineering may need to approve an alternative use, and production planning needs the accepted requirements and availability dates.
Review the classes at a cadence that fits the production cycle, and revisit important items when demand, product design or supply changes. Track whether the actions reduce unwanted stock without creating shortages. A bigger N category is not, by itself, evidence of better inventory control.
FSN versus ABC, XYZ and inventory aging
These analyses can complement one another because they ask different questions:
| Analysis | Main question | What it adds to an FSN decision |
|---|---|---|
| FSN | How actively has this item been consumed? | Directs movement-based replenishment and review attention |
| ABC analysis | Which items account for the greatest annual consumption value? | Shows the financial importance of usage, not just its frequency |
| XYZ demand analysis | How variable or intermittent is demand? | Helps distinguish steady consumption from irregular requirements |
| Inventory aging | How long has the stock still on hand been held? | Identifies old remaining batches even when the item continues to move |
A fast-moving item can still contain an old batch. A slow-moving item can have high annual consumption value. Selecting which SKUs to retain in the product range is another decision again; it needs customer and product considerations beyond a movement label.
Use the additional analysis when it changes the action, rather than building a large classification matrix nobody maintains.
Connect material decisions to a workable SkyPlanner schedule
The inventory review tells you what to replenish, retain or make available. Production still needs to know when the related work can run alongside everything else you have promised.
Imagine the team confirms that a slow-moving plate can be used for an approved order. Having the plate does not create a free machining slot. That order may compete with a regular bracket job on the same machine, and both may need a later assembly operation. Advancing one to use stock can delay the other.
SkyPlanner APS brings the accepted work, materials and capacity into one production schedule. With “Consider the materials” enabled, it accounts for availability at the operation that consumes the material. Purchase-order delivery dates represent expected availability; confirming a purchase order as Delivered updates stock when the material arrives.
Arcturus, SkyPlanner’s scheduling AI, fits operations to configured workstations, shifts, durations, dependencies and priorities. The Gantt view shows the resulting sequence and completion dates. Instead of separately adjusting a material list and several machine queues, you can review the production consequence in one plan.
You decide the business priorities. An S or N classification does not automatically make an order urgent, and an inventory-reduction objective should not silently override a delivery commitment. SkyPlanner handles the scheduling calculation around the priorities and constraints you set, reducing the manual work of keeping those decisions aligned.
That connection between materials and daily scheduling matters in practice. Before SkyPlanner, contract machining company Eskomatic organized work queues largely by hand, with limited visibility into material availability. Its team now uses a clearer Gantt work queue and automatic load scheduling. In its SkyPlanner review, Eskomatic reports more accurate delivery-date setting and fewer production stoppages caused by material shortages. The practical gain is seeing material readiness alongside the work it affects, early enough to make a better plan.
SkyPlanner integrates with any ERP or MES through its open REST API. You can keep your existing order and material systems while giving production a schedule that connects those decisions to actual capacity.
To see the difference, book a SkyPlanner demo around a regularly consumed component, a rare critical part and the approved jobs competing for the same machine. The useful question is not just which letter each part receives, but what the agreed action means for production and delivery dates. If you prefer to explore first, try SkyPlanner with demo data or the AI-assisted Getting Started in SkyPlanner Assistant.
Jussi Mäntylä
Production Planning Specialist, SkyPlanner


